How to source electronics from Shenzhen: the decisions that decide your quality
Sourcing from Shenzhen is not one decision, it is six — category, components, tolerances, factory, payment milestones, inspection. Most buyers only get to think about the first and the last. This is what happens in between.
Sourcing electronics from Shenzhen works when you verify three things before paying: who actually makes the product, what the unit cost covers, and how quality will be checked before shipment. But those three are only the gate. What separates a good order from an expensive lesson happens earlier — in the category you pick, the components you specify, and the tolerances you write on the drawing. Get those wrong and no inspection at the end will rescue you; a pre-shipment check can only confirm that the wrong thing was built correctly.
Why Shenzhen still wins — and what "Shenzhen" actually means
Shenzhen is the densest consumer electronics supply chain on the planet. But the phrase "a Shenzhen factory" is misleading, because almost nothing is made in one place. What you are really buying is a supply chain that fits inside a two-hour drive.
The division of labour in the Pearl River Delta is fairly stable, and knowing it saves you from asking the wrong supplier for the wrong thing:
- Shenzhen — design houses, reference-solution vendors, sourcing and export. Most of the engineering, the firmware, and the sample-making happens here, even when the mould is somewhere else.
- Dongguan — tooling, injection moulding, precision metal and plastic parts, and a lot of the final assembly. If your product has a housing, this is usually where the mould lives.
- Huizhou — battery packs and PCB fabrication, and a fair amount of larger-scale assembly.
- Guangzhou and Foshan — acoustics, speakers and home electronics, with a deep bench of transducer and cabinet suppliers.
- Zhongshan and Zhuhai — hardware, small appliances, and the accessory tier that feeds packaging and mounting.
Practically, that means a single product can touch four cities before it ships. The chipset and the reference firmware come from Shenzhen. The housing is moulded and painted in Dongguan. The cell is made in Huizhou. The driver is sourced from Guangzhou. Somebody has to own the handoffs, because the handoffs are where products get delayed.
Here is the part most overseas buyers do not see: the factory you talk to is often not the factory that runs every process. Between 30% and 60% of the process steps on a typical TWS earbud — plating, printing, coating, sometimes the driver itself — is subcontracted. Everyone in the chain knows this. Almost nobody volunteers it.
Three things to verify before you pay
1. Who actually makes the product
Ask whether the supplier is the manufacturer or a trading company. Both are legitimate, but you need to know which one you are dealing with. A trading company offers convenience and English communication; a factory offers lower pricing but expects you to manage the process. The most common failure mode is paying factory pricing and getting trading-company service — or the reverse.
A quick way to tell: ask to see the tooling records for a product they claim to make. A trading company will either not have them or will produce them slowly. A factory will know the mould number, the cavity count, and the day the mould was last serviced.
2. What the unit price covers
Confirm whether the quote is EXW (you arrange shipping), FOB (port), CIF (port-to-port), or DDP (door-to-door, including duties). Confirm packaging tier — basic polybag versus retail gift-box changes the price meaningfully. Confirm whether certificates (CE, FCC, RoHS, UN38.3) are included, and whether the test reports are in your company name or the factory's.
That last point matters more than people expect. A CE report issued to the factory is the factory's document. If you later move to a different supplier, or if a customs officer asks who placed the product on the market, you want the paperwork to point at you.
3. How quality will be checked before shipment
For orders above 1,000 pcs, an AQL-based pre-shipment inspection is standard. Agree the AQL level (commonly 1.5 / 2.5 / 4.0), agree which defects are critical / major / minor, and agree what happens on a failed inspection — rework, partial shipment, or full cancellation. Put it in writing before deposit.
Write the defect definitions yourself. "Slightly scratched" means one thing to you and another thing to a QC engineer trying to hit an on-time shipment. If you do not classify the defects, the factory will classify them for you, and every defect will turn out to be minor.
The category decides the supply chain
Before you negotiate anything, know how hard your product is to build. "Consumer electronics" is not one industry — the difficulty, the supplier pool and the failure modes differ sharply by category. This is roughly what we see across the categories we work in.
TWS and open-ear (OWS) earbuds — the easiest to start, the hardest to stand out
The most mature category by a wide margin. Reference designs and public moulds are everywhere, so a competent supplier can take you from brief to working sample in weeks. The catch is that everyone else can too. Differentiation does not come from the chipset, which is shared, but from tuning, fit, and packaging.
Bone conduction — the structure is the product
The transducer and the frame are the whole game. A bone conduction headset is a titanium or spring-steel band, a vibration unit, and silicone over both — the acoustic result depends on how tightly the band couples to the cheekbone. Water resistance is the other fork in the road: sports models live or die on sweat ingress, so the sealing design matters more than the driver.
Smart glasses — a much narrower supplier pool
This is where the assumptions of earbud sourcing break down. The optical engine (birdbath or waveguide) is its own supply chain, and it is not the same suppliers who make audio. The binding constraint is usually weight and heat: every gram in the temple arm competes with battery, and the display module needs thermal management that earbuds never needed. Far fewer factories can build a whole pair of smart glasses than can build a pair of earbuds.
Smart rings — small is not easy
Fitting a battery, an antenna, a PPG sensor and a PCB into a sealed ring under about 5 mm thick is genuinely hard, and yield is the reason the category stayed niche for so long. The antenna in particular fights the metal and the finger for space, which is why ring-to-phone reliability varies so much between suppliers.
Translation devices — hardware is the easy half
A translation earbud is mechanically an earbud with a microphone array. The difficulty sits in the language packs, the offline model, and the latency budget — none of which you can inspect by looking at the product.
One practical consequence: a factory that is excellent at TWS may be a poor choice for a ring or a pair of glasses, and vice versa. When a supplier tells you they can do all five, ask which one they actually ship in volume today. The honest answer is usually one, sometimes two.
Where the money and the risk sit in your BOM
Buyers tend to focus on the headline chipset. In practice the components that decide whether customers are happy sit elsewhere.
The main SoC
The Bluetooth SoC sets your version support (5.3, 5.4, LE Audio), whether active noise cancelling runs on dedicated hardware or drags the main core, and how much power is left for everything else. Two decisions live here: whether you take the vendor's reference firmware or pay for customisation, and whether the chip has a road map. Public reference designs move quickly; a firmware branch written for you does not, and you will own the maintenance.
The speaker driver
This is the component buyers most often under-specify, and the one customers judge instantly. Driver diameter (6 mm, 10 mm, 13 mm and up), diaphragm material, magnet strength and suspension all shape the result — two earbuds with identical chipsets can sound like different products because of the driver and the front cavity behind it. Sensitivity matters as much as the frequency curve, because it determines how loud the product is at a given power budget.
The battery
Almost every wearable in this sector runs on a lithium polymer pouch cell, chosen for shape flexibility. What differs is the protection board, the cycle life, and whether the cell has passed UN38.3 — the transport test that governs whether it can fly. A cheaper cell with a thinner protection circuit is the single most common source of returns and, occasionally, safety incidents. There is no version of this where saving money on the protection board is a good trade.
The sensors and the microphone array
If the product claims health features, the optical front end and the mechanical design around it decide whether the numbers mean anything; a heart-rate reading is only as good as the contact between the sensor and the skin. On the audio side, the number of MEMS microphones and where they sit determines how well environmental noise cancelling works — two mics is a baseline, three or four is where beam-forming starts to matter.
Our own position on this: do not treat the driver and the battery as places to find margin. They are the two components a customer notices within a minute and the two that generate warranty claims. Spend the savings on packaging instead — packaging is where a cheaper decision actually goes unnoticed.
Tolerances and materials: where cheap gets expensive
Drawings are where inexperienced buyers lose the most money, because a tolerance is a price. Tighten it for no reason and you pay; leave it open and you get a product with visible gaps.
The default for consumer electronics is ISO 2768-m, the medium class. It is fine for non-mating surfaces. For anything that has to line up — the seam between two halves of a shell, a button in its channel, a lens in its bezel — you want the fine class, ISO 2768-f, or an explicit callout. What matters most is understanding accumulated tolerance: five parts each held to plus or minus 0.2 mm can stack into a one-millimetre gap on a finished assembly. The gap is not any single supplier's fault. It is the drawing's fault.
Surface finish follows the same logic. Spray painting is the cheapest and the most sensitive to dust. Electroplating gives a hard metallic look but hides nothing on the mould. In-mould labelling puts the graphic inside the plastic and eliminates wear, at the cost of tooling complexity and a longer first article. Anodised aluminium looks great and scratches permanently.
Water resistance is not a coating — it is a mechanical design. IPX4 is splash resistance and is mostly about geometry: water must not be able to sit on a seam. IPX7 (submersion at one metre for thirty minutes) requires a real seal, typically an O-ring or a gasket combined with ultrasonic welding of the housing. The move from IPX4 to IPX7 is not a percentage increase in cost; it is a different product architecture with a different tooling set.
Material choice usually comes down to a handful of trade-offs. ABS is cheap, easy to mould and easy to scratch. Polycarbonate takes impact and costs more. PC/ABS blends are the usual compromise for shells. TPU and silicone are for anything that touches skin. And for rings, titanium and stainless steel are the only options that survive daily wear without deforming — which is exactly why the category took twenty years to get cheap.
How to judge a factory in one visit
You cannot verify a supplier from a catalogue and you usually cannot spend a week on site. What you can do is know which six things to look at, because in a working factory none of them can be faked quickly.
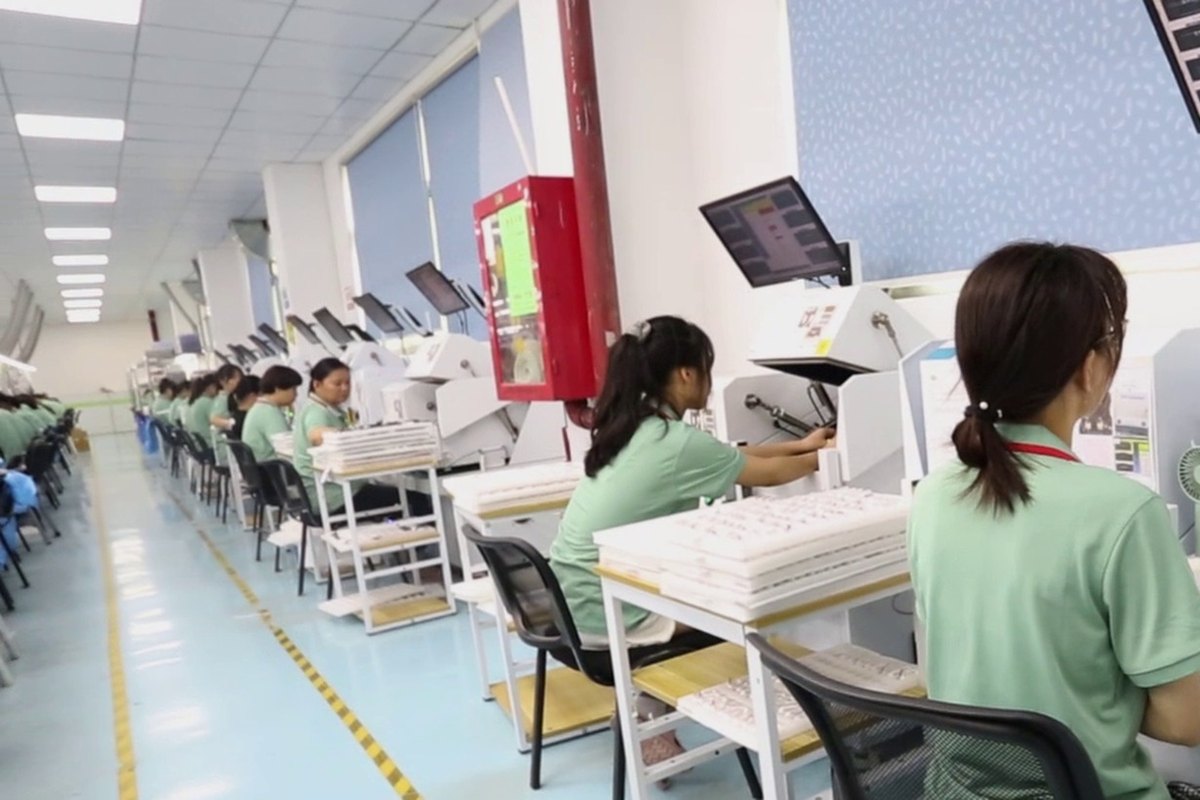
Our method is four stages, and the order matters:
- Screen — look at what they make, not at what they say they make. Ask for three customers in your category, then ask which factory each of those products was built in.
- Lock — establish who owns the tooling, how much capacity is genuinely available to you, and which processes are outsourced. Tooling ownership is the single most important commercial detail in an OEM relationship; if you do not own the mould, you do not control your product.
- Process — review incoming material inspection records, the test stations on the line, and whether there is an ageing or burn-in step. Ask to see today's records, not a file prepared for visitors.
- Deliver — check that packaging has a signed golden sample, that the inspection standard is written down, and that export documents are correct. A perfectly built product with the wrong label on the carton is still a failure.
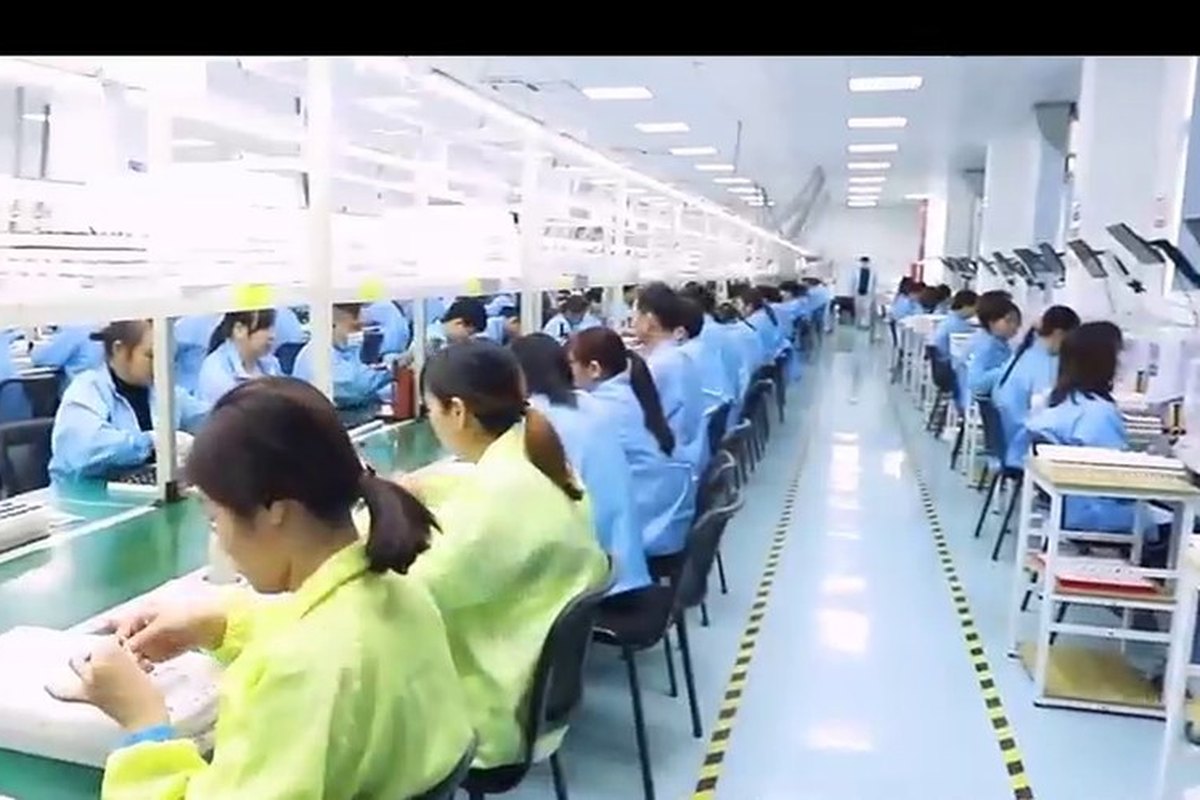
On site, the six things worth your time: the tooling store, the incoming-inspection bench, the line test stations, the ageing room, the packaging area, and the finished-goods warehouse. If a factory will not show you one of these, that is the answer to your question.
We keep our partner list private and our method public. The reason is simple: naming suppliers helps our competitors, while explaining how we qualify them helps our customers. Those are not the same thing.
Payment milestones that keep both sides honest
The most common structure for first orders: 30% T/T deposit on PO confirmation, 70% balance against pre-shipment inspection report. This means the factory gets funded to start production, and you get a real checkpoint before the final payment clears.
For repeat orders with an established relationship, net-30 or net-60 against shipment is common. Do not extend payment terms too early — the factory has cash flow just like you do, and a supplier that is short of cash makes decisions you will not enjoy.
One thing worth insisting on regardless of the terms: the inspection report must be issued before the balance is due, not after. If payment and inspection happen on the same day, the inspection becomes a formality.
Common pitfalls
- Skipping samples. A $100–$300 sample fee is cheaper than a $10,000 misunderstanding.
- Trusting glossy catalogs. Many factory catalogs borrow photos from other factories. Verify with a video call or on-site visit.
- No NDA on custom projects. Before you share unique design or firmware, sign a mutual NDA.
- Last-minute spec changes. Every change after production starts costs time and money. Lock specs before deposit.
- Specifying a tolerance you cannot explain. Every callout on the drawing is a cost. If you do not know why a dimension is tight, neither does the factory — and you will pay for the tightest interpretation.
- Treating the certificate as the product. A CE or FCC report confirms the sample passed the test. It says nothing about whether unit 4,000 will. That is what AQL inspection and process control are for.
Two of those pitfalls deserve a longer answer than a list can carry. Judging a factory in one visit is a method rather than an instinct — the 12 checks we make before onboarding a plant is the version we use. And the gap between a certificate and a controlled process comes down to how the goods are sampled, which reading an AQL inspection report covers in detail.
Don't want to manage this yourself?
We coordinate the full flow with vetted Shenzhen partner factories — sourcing, component selection, tooling ownership, QC, export paperwork, NDA-protected OEM. We usually reply within one business day.
Send an inquiry →